KSB: more than 150 years of innovation in fluid engineering
Find out why KSB equipment is the global standard in fluid engineering and how first-class technology delivers higher operational efficiency and lower long-term costs, through Techworks, your authorised distributor in Romania.
KSB: more than 150 years of innovation in fluid engineering
When it comes to industrial processes, water treatment or complex installations, equipment reliability is not optional. Founded in 1871 in Frankenthal, Germany, KSB has grown from a visionary business into a world leader in the manufacture of pumps, valves and related systems.
With a presence in more than 100 countries, 35 production sites worldwide and more than 16,000 specialists, KSB has redefined quality standards, supplying equipment designed for the harshest and most demanding operating environments.
Techworks: official KSB distributor in Romania
Choosing premium equipment requires a partner to match. As the official KSB distributor in Romania, Techworks gives local industry direct access to German engineering. We do not just deliver pumps, but complete technical solutions that ensure operational safety.
The main benefit for the user is lower long-term maintenance costs (TCO). With Techworks' technical expertise, every piece of KSB equipment is correctly sized and selected, ensuring a continuous process with no production downtime.
Why choose KSB equipment over generic solutions?
The market is flooded with generic pumping solutions that attract with a low initial cost but cause heavy losses through inefficient energy use and frequent failures.
KSB equipment combines new technologies, advanced hydraulic design and high-performance materials. This sets it clearly apart from the rest of the market: minimal mechanical wear, maximum hydraulic efficiency and full protection against corrosion and aggressive media.

Advantages of KSB pumping systems
- Higher operating efficiency: Maximum flow rate with low energy consumption.
- Minimum life cycle costs (TCO): Infrequent maintenance and long service life.
- Continuous innovation: Built-in monitoring technology to prevent premature wear.
- Guaranteed quality: Production certified to the highest industrial standards (ISO 9001, ISO 14001).
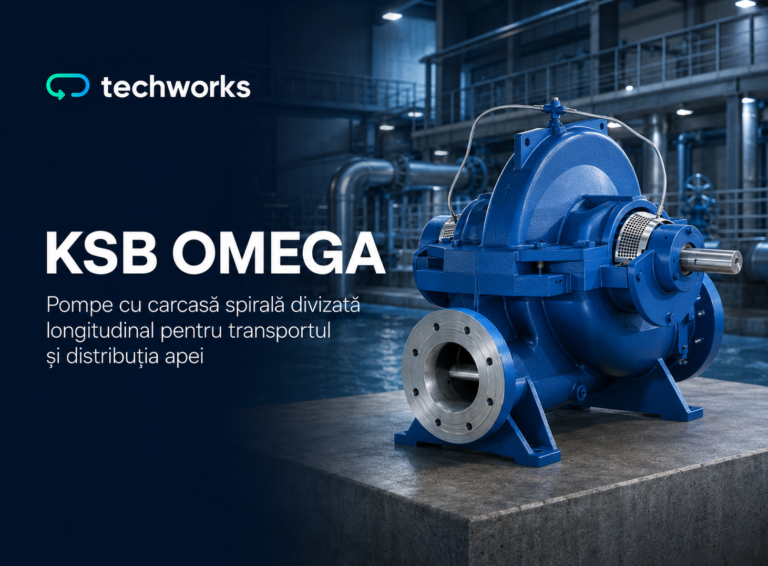
- Versatility: A very wide range of solutions, from the global standard Etanorm to complex pumps for chemical media.
Sustainability and environmental standards
KSB innovates not only for performance but also for the future. KSB pumps and systems are designed to meet the strictest sustainability standards. Through hydraulic optimisation, the equipment saves hundreds of thousands of tonnes of CO2 a year worldwide. In addition, KSB production lines in Europe use a growing share of renewable energy, showing a real commitment to environmental protection.
KSB equipment applications
The KSB pumps and solutions distributed by Techworks are essential in:
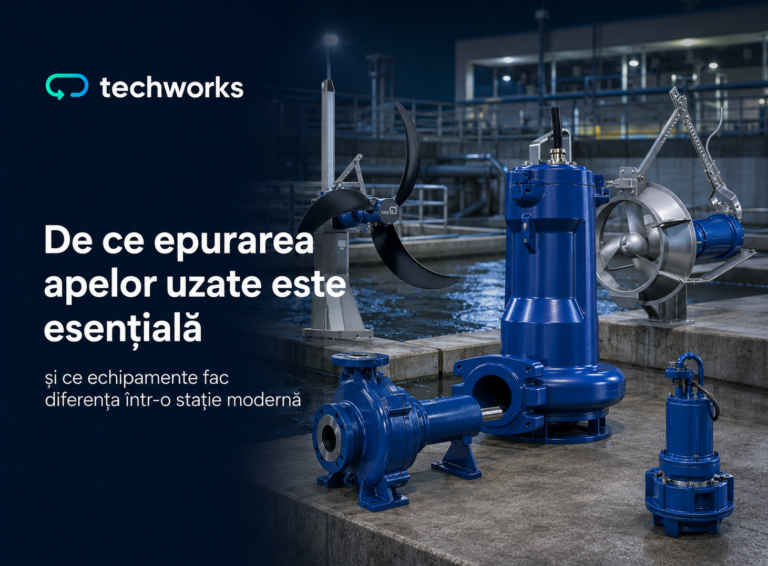
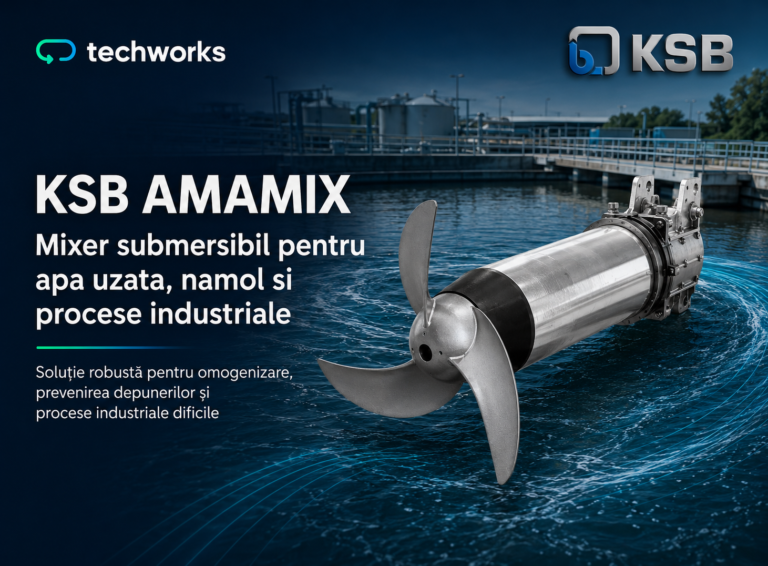
- Water treatment and wastewater treatment plants
- Energy and district heating
- Chemical and petrochemical industry
- Food and beverage industry
- Construction, office buildings and HVAC systems
KSB brand FAQ
What sets a KSB pump apart from other brands on the market? KSB pumps stand out for their long service life, top-class hydraulic design that substantially reduces energy consumption, and German material quality.
Is KSB equipment suitable for corrosive media? Yes. KSB makes special ranges of pumps and valves in advanced materials and alloys, designed specifically for aggressive fluids and heavy industry.
Where can I buy genuine KSB products in Romania? Through Techworks, the official authorised distributor. We provide correct equipment selection, technical support and a guarantee of authenticity.
Move to German efficiency
Choosing a world leader such as KSB means operational reliability, consistent performance and lower costs. Do not let inefficient equipment set the pace of your production.
Contact the Techworks team for specialist technical advice, request a tailored quote for your project or browse the KSB product range on our website.
Read also: KSB Pumps in the Food Industry: How to Reduce Costs