KSB pumps in the food industry: how to reduce costs

When KSB pumps are used in the food and beverage industry, production continuity and hygienic safety are critical. But operating costs are rising. Maintenance managers face a new challenge: how do we keep the same quality standards while reducing the energy bill? The answer lies not in complex control systems but in the basic efficiency of each individual unit.
The challenge: oversized pumps and wasted energy
A common problem in production facilities is the use of oversized pumps “to be safe”. According to industry data, a very large share of plant pumps do not operate at the Best Efficiency Point (BEP). The result? Significantly higher energy consumption. Added to this is premature wear of mechanical components, caused by vibration and unbalanced internal pressures.
Correct sizing: savings of up to 30% and hygienic standards
The first step towards optimisation is selecting the right pump for the specified fluid (from viscous liquids such as syrups or dairy products to process water). The Techworks team ensures that every KSB pump integration in the food industry is sized exactly to your installation's actual requirements.
Precise hydraulic sizing that brings operation as close as possible to the BEP can deliver energy savings of up to 30%, eliminating the unnecessary losses caused by unsuitable equipment.
In the food industry, internal design is also crucial. Equipment from dedicated ranges, such as KSB Vitacast, are designed with virtually no dead zones (“no dead volume”). This allows cleaning and sterilisation in place, in strict compliance with CIP/SIP (Cleaning in Place / Sterilisation in Place) standards, which are vital for food safety.
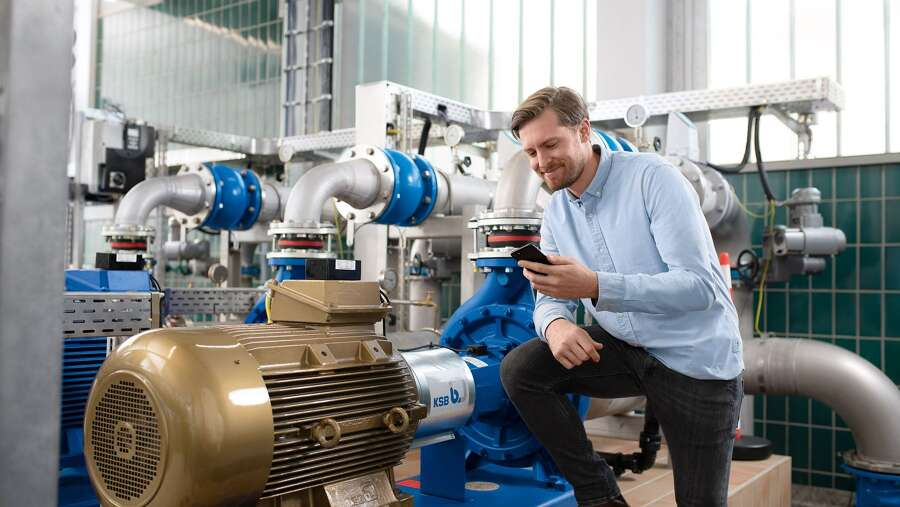
Performance monitoring: predictive maintenance without complex automation
To maintain efficiency over the long term, Techworks focuses on active monitoring of operating parameters. We do this without adding complex automation systems or direct flow control equipment, simply by analysing actual operating data.
Using dedicated technologies such as the monitoring sensors KSB Guard, we can continuously track vibration levels and equipment temperature. This monitoring-only approach offers major advantages:
- Preventing failures: We identify anomalies early, before they cause a sudden shutdown of the production line.
- Controlled operating costs: With clear data, you can plan maintenance work exactly when it is needed and avoid emergency repairs (which are always the most expensive).
Frequently asked questions about these KSB pumps in the food industry
What is BEP and why does it matter? BEP (Best Efficiency Point) is the operating point at which a pump runs at maximum hydraulic efficiency. Operating at this point minimises energy consumption and radial forces, substantially extending equipment life.
Do KSB pumps meet food industry standards? Yes. Dedicated models (such as the Vitacast series or hygienic lobe pumps) are made of high-grade stainless steel and are specifically designed for full compatibility with CIP/SIP cleaning procedures.
Is plant automation required to prevent failures? No. With proper monitoring of vibration and temperature sensors, predictive maintenance work can be planned very efficiently, without the need for automated control of the entire pumping line.
Why work with Techworks?
As the official distributor in Romania, Techworks provides specialist technical advice to make sure your investment in KSB equipment is justified by real long-term reliability.
Are you sure your current pumps are running at maximum efficiency? Contact the Techworks team for an analysis of your system and find the right pumping and monitoring solutions for your plant.